Jaguar Land Rover Trials Drones To Cut Inspection Time By 95% At EV Facility
- By MT Bureau
- December 04, 2025
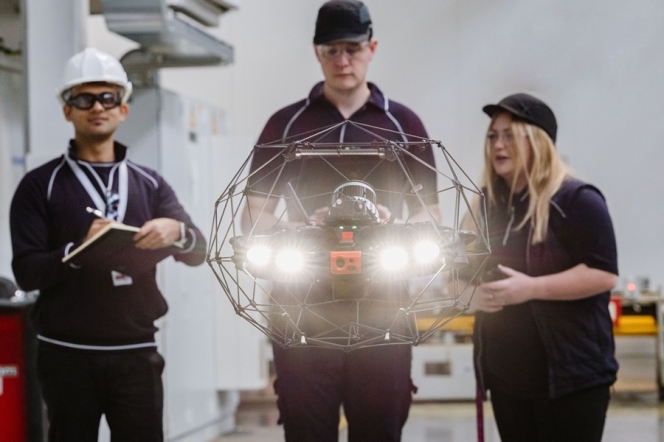
Tata Motors-owned British marquee luxury brand Jaguar Land Rover (JLR) is trialling drone technology at its Electric Propulsion Manufacturing Centre (EPMC) in Wolverhampton, successfully reducing machinery and site inspection time by up to 95 percent. The pilot is an important step forward in operational efficiency and employee safety, aligning with JLR's vision for its factories of the future.
The Elios 3 drone by Flyability reaches high and confined spaces, allowing maintenance teams to inspect equipment safely from the factory floor, eliminating the need for elevated platforms and reducing risk. Operated via tablet, the drone delivers a live 3D map to identify and troubleshoot issues. This helps JLR prevent costly maintenance downtime while freeing up employees’ time for business tasks.
The drone uses Light Detection and Ranging (LiDAR) sensors to create detailed 3D maps of the surrounding environment. Additionally, it features a thermal camera to help pinpoint overheating components or insulation failures, helping optimise energy use by detecting inefficiencies early and supporting JLR’s efforts to reduce its overall operational emissions.
Nigel Blenkinsop, Executive Director of Industrial Operations, Jaguar Land Rover, said, “As we transform our facilities, we’re rethinking every part of our factories, including how we maintain and operate them. Trials like this one with advanced drone technology are helping us improve employee safety, reduce maintenance downtime and operate more efficiently. Just as importantly, they’re helping upskill our people in the latest digital technologies, ensuring our teams are part of our factories of the future.”
Shantnu Mehta, Project Engineer, Jaguar Land Rover, said, “I never imagined I’d be learning to fly drones as part of my role. It’s been exciting to learn how to use this technology and the skills I’ve developed will stay with me throughout my career. Being part of such an innovative project and contributing to how we’re transforming our factories for the future is something I’m genuinely proud of.”
Following successful trials at EPMC, the next phase will take place at JLR’s Logistics Operations Centre (LOC) in Solihull – a vast warehouse space equivalent to thirteen football pitches (approx. 91,800 square metre). Here, the drone will be equipped with barcode scanners to automate inventory checks, replacing manual processes and enabling faster, accurate stock updates. This will help improve safety, reduce errors, and support smarter decisions on space, stock levels and supply flow.
The initiative is part of JLR’s GBP 3.8 billion annual investment into industrial transformation, new products and technology, and is being explored through its Open Innovation programme. It also supports JLR’s Future Skills programme, which aims to train 29,000 employees in electrification and digital skills.
- Audi AG
- Audi A2 e-tron
- Ingolstadt
- Audi A3
- Gernot Dollner
- Jorg Schlagbauer
- Gerd Walker
- Siegfried Schmidtner
Audi Commences Production of A2 e-tron At Ingolstadt Plant
- By MT Bureau
- September 11, 2026

German automotive luxury brand Audi has started series production of the all-electric A2 e-tron at its main plant in Ingolstadt, Germany.
Interestingly, the company claims that the development timeline for the A2 e-tron was reduced by 21 months compared to previous vehicle projects through streamlined pre-series evaluation and coordination processes. The EV manufacturing process incorporates structural changes to lower operational complexity.
Audi implemented the string-of-pearls production sequence at Ingolstadt, fixing customer order sequences six days prior to assembly. This system allows component suppliers to deliver pre-sorted parts directly to the assembly line, eliminating regional storage and component sequencing areas.
The body of the A2 e-tron is assembled on shared line infrastructure alongside the Audi A3, utilising more than 1,200 reallocated components and 250 repurposed welding robots. Automated systems include camera-guided bin-picking robots for small sheet-metal parts and fully automated wheel installation stations replacing semi-automated bolting in chassis preassembly.
On the digital infrastructure side, the plant runs the Edge Cloud 4 Production platform, which centralises the control units for vehicle commissioning and operator guidance systems, replacing over 450 industrial PCs in the assembly area.
The facility also uses artificial intelligence assistants, including supply chain and maintenance chatbots, to assist line personnel with fault diagnostics and documentation retrieval.
Gernot Dollner, CEO, Audi AG, said. "The Audi A2 e-tron represents the next step in our renewal. It shows how we consistently think from the market backward, because different regions need different answers. The A2 e-tron was developed for Europe and is manufactured in Ingolstadt. It is the most efficient Audi we have ever built, and it makes electric mobility suitable for everyday use. At the same time, it shows how we are implementing our transformation in concrete terms: developing faster, producing more efficiently, and thereby strengthening industrial value creation and competitiveness in Germany."
Jorg Schlagbauer, Chairman, Audi General Works Council, said, "The start of production of the A2 e-tron in Ingolstadt is a strong signal for our site and its future. We are particularly proud of this as the works council, because together with the workforce we have repeatedly fought with great determination since 2019 for Audi to develop an entry-level electric model and build it in Ingolstadt. The project stands for technological expertise, industrial value creation, and secure prospects for our employees. Above all, however, the successful production launch is the result of the tremendous commitment and skill of our colleagues. Once again, this shows: at Audi, Vorsprung durch Technik is not just announced, it is achieved."
Gerd Walker, Board Member for Production and Logistics, Audi, said, "The A2 e-tron again demonstrates that it is possible to build cars profitably in Germany. Particularly important in this regard are AI assistants developed jointly by our Neckarsulm and Ingolstadt sites, our highly flexible production facilities, and, above all, the expertise of our employees. The model demonstrates the transformation of Audi production: less complex, even more efficient, and with a high degree of digitalisation and automation."
Siegfried Schmidtner, Plant Manager at Audi Ingolstadt, said, "The start of production of the Audi A2 e-tron is the result of extensive teamwork at the Ingolstadt plant. Drawing on their wealth of experience from numerous product launches, the team has laid the groundwork for a successful ramp-up of the model and further optimised our processes. Production of the new model strengthens core capabilities at our headquarters."
The site prepared its workforce for the launch through a multi-stage qualification program combining traditional assembly line instruction with virtual reality training modules.
LICO Partners Epsilon Advanced Materials For Battery-Grade Graphite Recovery
- By MT Bureau
- September 10, 2026
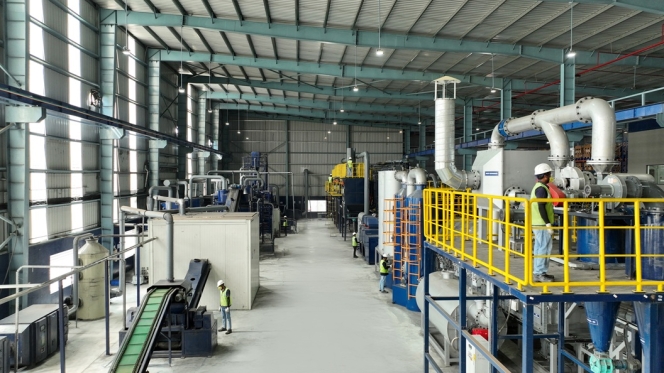
LICO Materials and Epsilon Advanced Materials have established a supply agreement to recover graphite from end-of-life lithium-ion batteries and cell manufacturing scrap for use as secondary feedstock in battery anode production.
Under the partnership, LICO Materials will process battery waste and manufacturing scrap using its mineral recovery technology to isolate graphite. The material will be supplied to Epsilon Advanced Materials for qualification and integration into its synthetic, natural, and blended graphite anode production platforms. Product samples from the recovered feedstock will be distributed for customer testing by the end of 2026. Graphite constitutes 20 to 30 percent of a lithium-ion battery's weight.
At present, China controls over 90 percent of global graphite refining and anode material production, with International Energy Agency projections indicating China will supply 80 percent of battery-grade graphite through 2035. India's Ministry of Heavy Industries projects domestic lithium-ion battery demand to reach 210 gigawatt-hours by 2030, requiring 200,000 to 230,000 tonnes of graphite anode material annually.
Gaurav Dolwani, CEO and Founder, LICO Materials, said, "Graphite is a critical material for the battery industry, yet its supply chain remains highly concentrated in China. Recovered graphite gives us an opportunity to retain material that is already within the battery ecosystem and return it to productive use. Supplying this recovered graphite to Epsilon Advanced Materials marks a breakthrough in our journey beyond battery recycling and brings us closer to closing the graphite loop."
Vikram Handa, MD, Epsilon Advanced Materials, said, "As global battery manufacturing expands, diversifying sources of graphite has become increasingly important. Recovered graphite provides an opportunity to complement conventional feedstocks while retaining valuable material within the battery ecosystem. Our work with LICO creates a pathway to bring recovered graphite back into advanced anode material production and strengthens the circularity of the battery materials value chain."
The agreement establishes domestic secondary feedstock sourcing for battery anode production, reducing reliance on primary graphite imports as Indian battery cell manufacturing expands.
Ultraviolette To Build 250,000 Units Per Annum Capacity BIGGA Factory In Hosur
- By MT Bureau
- September 10, 2026
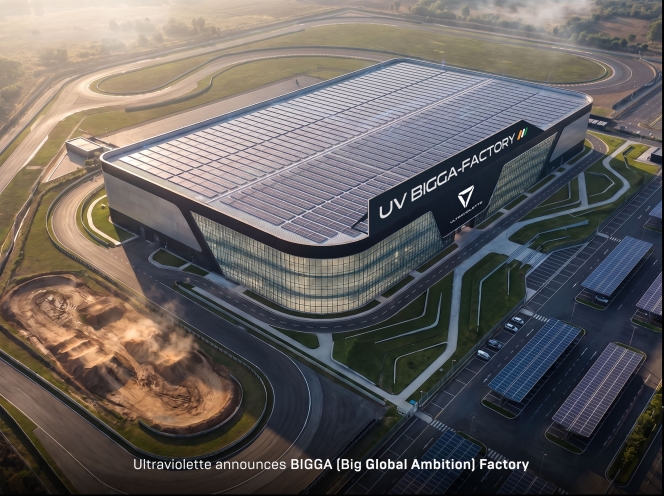
Bengaluru-based electric vehicle maker Ultraviolette Automotive has announced plans to establish a new manufacturing facility – the BIGGA Factory – in Hosur, Tamil Nadu. The plant will manufacture the Tesseract electric scooter and support the company's future product portfolio across sports, crossover, cruiser and street motorcycle segments.
The facility, located at the SIPCOT Industrial Park in Shoolagiri, will feature an initial production capacity of 250,000 units per year, which can be scaled up to 500,000 vehicles annually.
The site will complement Ultraviolette's existing plant in Bengaluru, Karnataka. The project is expected to generate approximately 2,000 jobs during its first phase.
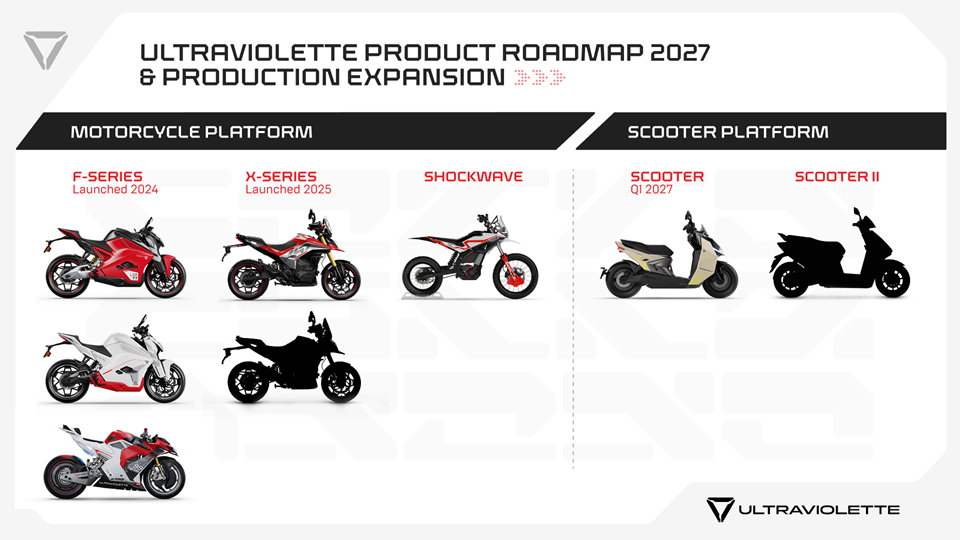
The manufacturing setup will integrate Industry 4.0 systems, a Manufacturing Execution System for real-time tracking, collaborative robots for welding and assembly and vision-based inspection tools. The facility will also include an on-site test track to evaluate completed vehicles prior to delivery.
Narayan Subramaniam, Co-Founder and CEO, Ultraviolette Automotive, said, "We are at an inflection point in Ultraviolette's journey. Over the last few years, we have built our foundation around technology, performance and product innovation; the next phase is about building the scale to take that foundation much further. The BIGGA Factory is a significant step in that direction, giving us the manufacturing capacity and infrastructure to scale Tesseract and our future products, while creating the ability to serve a much larger customer base in India and international markets. Our current facility in Bengaluru, Karnataka will continue its regular operations alongside the BIGGA Factory, strengthening our long-term manufacturing and technology footprint in India."
Niraj Rajmohan, Co-Founder and CTO, Ultraviolette Automotive, said, "Hosur is a key manufacturing hub with a well-established automotive ecosystem, significant supply-chain advantages and close proximity to Ultraviolette's R&D operations and existing supplier network. These strategic advantages, combined with the scale, precision and manufacturing agility of the BIGGA Factory, will enable us to deliver the Tesseract and our future products to customers in India and international markets while maintaining the highest standards of quality and performance. The BIGGA Factory will further strengthen our ability to innovate and contribute to India's emergence as a global hub for electric-vehicle technology and manufacturing."
Vedanta Invests Over INR 210 Billion To Build India’s EV Metals Ecosystem
- By MT Bureau
- September 09, 2026
Vedanta Group has announced that it has invested over INR 210 billion through FY2026 across projects to expand production capacity for aluminium, zinc, value-added alloys, copper, steel, nickel and ferrochrome. The capital deployment aims to scale domestic material production, supporting India's electric mobility and automotive sectors.
The investment addresses rising national demand for vehicle electrification components, including battery cells, energy storage units, electric motors, power electronics, semiconductors, charging infrastructure and vehicle structural parts.
At present, India imports over 80 percent of its critical mineral requirements. To establish domestic resource access, Vedanta said it has secured 10 critical mineral blocks covering copper, nickel-chromium-platinum group elements, tungsten, graphite, vanadium, rare earth elements and potash, with exploration activities active across five of the sites.
Within its metals operations, Vedanta Aluminium Metal produced 2.45 million tonnes of primary aluminium during FY2025–26. The division supplies primary foundry alloys, rolled products, billets, and slabs for automotive applications, alongside low-carbon offerings under its Restora and Restora Ultra product lines. The group is expanding smelting and value-added alloy capacity at its plant locations in Chhattisgarh and Jharsuguda, Odisha.
In battery materials, Vedanta operates as India's sole primary nickel producer. Through its subsidiary Hindustan Zinc, the group produced 851 kilotonne of refined zinc and 627 tonnes of saleable silver in the 2025–26 financial year, offering automotive zinc alloys and its low-carbon EcoZen product line. For electrical applications, Vedanta Limited reported cathode copper production of 170 kilotonne over the same period, while expanding downstream processing capabilities via a copper rod facility in Saudi Arabia.
Arun Misra, CEO, Vedanta Group, said, "As EV adoption accelerates, the strength of India’s journey will increasingly depend on its ability to secure reliable access to the metals and critical minerals that underpin vehicles, batteries and charging infrastructure. Building these capabilities domestically will be essential to creating supply chains capable of supporting India’s long-term mobility ambitions. At Vedanta, we are investing across this opportunity through our presence in key metals, while building capabilities in critical minerals. We are expanding our role across the resource base that will support the next generation of mobility and battery value chains."
Comments (0)
ADD COMMENT