Hyundai Motor India’s Manufacturing Excellence Turns Metal To Marque Cars
- By 0
- April 05, 2020
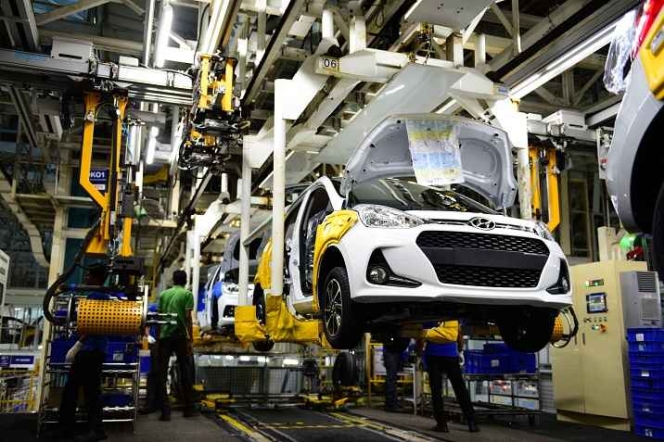

HMI has 2 plants, established in 1998 and 2007. In the last 5 years both the plants have been augmented for capacity enhancement. This was possible as the assembly lines were initially designed for flexibility in augmentation, expanding to the needs of the following 15-20 years. That has always been the philosophy of Hyundai which is really paying off now; it becomes easier to execute improvements in all their projects.

Consider the body shop where components are accumulated to be worked upon. It is built on global bodyline concepts. Not only volume escalation but also increase in the number of models can be managed effectively. Every day the plant processes 395 tonne of steel coils, globally monitored by ‘Die Management’ system, to make cars with each one having on an average 4,500 spot weldings done by 4th gen robots. So far the company has manufactured more than 9 million cars using steel coils having a length that could cover the circumference of the earth 4 times. The intelligent weld management system generates about 30.6 million data points per day and the quality is controlled through real-time monitoring. Beginning with making one car every 4 minutes in 1998, the plant currently rolls out a car every 33 seconds.
Ganesh Mani S, Director, Manufacturing, HMI, told Motoring Trends that “we have 12 models now with 350 internal variants. The complexities in these are double challenges for us especially when we take to the next level. We were able to manoeuvre 3 or 4 models 3-4 years ago from a single line. Now it is 7 models. Volumes have also increased from 49 to 66 UPH (unit per hour). We have a two-pronged strategy; one is adding on volumes that can cater to the needs of consumers and, two, the capability for enhancement. Since we have our own Factory Automation companies in the automotive hub of South Korea, we have gone from Generation-1 to Generation-4 of robotics, which brings in a certain amount of flexibility and increase in the speed of execution. With CAFE and other norms, we need to make a model that is robust, which comes from the basic design and the way we build the product.”
Body shops are by and large 100 percent automated and therefore, the company was able to make them intelligent enough to understand, with the fourth generation robots. For every vehicle it is necessary to have resistant spot welding and for every spot there is a specification; this needs to be modified for each new model. The company has introduced intelligent timer controls, which is called MMDI - in the line before spot welding, it checks the number of components and their thickness and the level of current and voltage requirements.
 Earlier they were pre-set, but now keep changing at every place. This gives twin advantages. The first is to have multiple components as technologies keep changing; aluminium may come in; high tensile steel welding has already come. At present the plant has about 400 robots with MMDI which have the capability to keep checking every time. Earlier it used to take 40 seconds to complete 30 spots; now within that TAKT time, it is able to make 50 spots increasing the speed of the line.
The second is having Intelligent Vision Control Systems. For instance, sealer has to be applied for vibration, harshness, noise, dust and rust prevention, strength, etc. The system monitors the route it has to follow and checks whether the job is being done properly or not. It ensures quality and traceability of the arrangement.
“Whenever we introduce a new model all we have to do is to make use of the carrier, a hardware that allows robots to move around and make the body parts. Only the carriers need to be replaced as the line operates depending on the types to be made. Earlier we had electric and pneumatic carriers to move across to lift the body and components while in the fourth generation robots at present the individual carrying capacity has been increased multiple times. The entire handling mechanism of conveyors, platforms, holding chains, etc has been replaced by just programming the robots which can handle them. All these save time and make the operation of the body shop more convenient,” he said.
 A robot has shelf life of approximately 7 years; as and when replacements are due, new technologies are incorporated into the system. With so much innovation in robotics, the cost of robots is going down. Over the years the company has garnered expertise to the extent that a new robot can be commissioned in 48 hours, when it is needed to augment capacity. The industry average is 7 or 8 days. The supervisors and technicians can do the programming themselves, which also saves cost. Assembly shops have seven or eight major equipment and the company has been able to change or enhance the equipment that is augmented with VFD (variable frequency drive) as and when required. A fall back mechanism is in place to manage demand fluctuations. Robotic multi-skills and flexibility switchover help the line to go on smoothly. When not required some of the robots can be kept in sleep mode to save energy. Like managing absenteeism of people with multi-skills some of the robots can double up while the others can rest.
On the scope for improvement in enhancing UPH, Ganesh Mani said, “We can manage with this arrangement till 2021. We change regularly our upgradation on various models and try to eliminate defects at the design stage itself. We have a team working on every model and the results are ploughed back at the design stage to remove deficiencies. Also, there is the influx of technology in terms of inspection and robustness of the process. ‘Before’ and ‘After’ is 100 percent mapped for the sealers so there is no question of missing and moving across to the next stage.”
 In the body shop the operator has all the available information in front of him. In the assembly shop everything is mapped digitally. The operator looks at a digital display to know which component he has to pick up; he also gets an audio message regarding assembly of parts for rare models. The company has created a Smart Innovation and Automation Team (SIAT) which is one step ahead in process monitoring to ensure that errors do not creep into the system; it makes certain that the operator does not commit a mistake. For instance the lid of containers holding the parts for the specific models will only open when required and at the right station.
Asked what happens if the operator has not taken the required number of parts like fasteners, he said, “We have more than 700 dynamic bolts and nuts that are fitted on the vehicle; any mistake in fitment would create havoc. We have HIVIS (Hyundai Integrated Vehicle Inspection System) which is a tool by itself. The torque values while tightening every nut are registered in the system. Any mistake made triggers an alarm and the vehicle will not be allowed to go to the next stage. The tightening process is monitored in real-time and is coupled with sign-off gate. When there is a process deviation, the system will not allow the car to roll out of the assembly line, thereby ensuring mistake-proof delivery. The system, developed at HMIL, is so intelligent that it is used all over the world. For example, when new trainees come, sometimes cross-threads happen; the torque goes very high and the value is reflected in the torque curve. This helps us take immediate corrective action. One of our engineers developed a ‘gyro metric gun’ that works on the straightness principle. It has a sensor inside, working on the principle of gravitational force; if there is any deviation of line it will not allow the operator to tighten the nut. This is a unique system, being used in all the 32 plants of Hyundai globally.”
 How can variability happen? It can happen because of improper training; the company has taken care of this. The other variability is fatigue that could set in and result in the operator making a mistake. To prevent this there is REBA - Rapid Entire Body-movement Analysis - that can calculate the fatigue level in the individual. This information would help improve his comfort level. Meticulous planning has been done for all the stations, upgrading them from category A (with possibility of over 12 risk occurrences) to category D (less than 4), to bring down the risk level. On this platform there are many assist systems for the operator. The company is working on EXO skeleton which is a human-machine interface where a vest is provided to the operator giving him, among other things, elbow support. This makes the process easier and lighter; consistency always gets measured.
Ganesh Mani explained, “We also have vision camera system robotics that can capture 70 frames per minute. It compares the pictures with the original and if there is an error sends the message within a TAKT time of 40 seconds. This is our third layer of inspection. By and large our pass ratio is 100 percent; it is only a fall-back mechanism.”
Though the number of models assembled in one line has substantially increased, the company hopes that it can increase further. In assembly, there can be a high of as many as 240 different models, the maximum in a single line, he pointed out.
However, when the UPH in the body shop is increased it has to match the TAKT time of the assembly line as well. “In a lean production system we don’t want too much of a cushion in the other shops as that would prevent hidden problems from coming out. So we don’t go beyond one additional UPH in the previous shop; in between we have some amount of stock for body storage. Within that we manage our line. Every hour the body shop can create 1 more additional body in the same time required for assembly. In this way we can manage any breakdown or process delay up to 1 UPH. On a cumulative of 22 hours that we run, everyday a cushion of 22 bodies will be available to help us manage any kind of change,” he said.

Industry 4.0
About the possibilities of a smart factory Ganesh Mani said, “As part of our agile manufacturing process in our technologically advanced and digitalised factory we wanted to use Industry 4.0 in a big way. Our initiatives for this have started. We have found out that earlier in a body shop alone close to 1GB of data was generated; today it is 15GB a year from all the modules put together. The next stage is to integrate the data seamlessly and put them on display so that the operator who is multi-tasking can see them easily and monitor them thoroughly. This also helps in predictive maintenance which is the objective of big data. We use this in a 6-8 hour slot on Sundays when the assembly line does not work. Any change can be made then. This phase pre-empts impending failures; we use infrared mechanisms to do this. We also have vibration sensors fitted in the equipment that constantly monitor and give an alarm if something is likely to happen like heating up of the motors. We have a Data Analytics Team that looks into all these and takes preventive action. Today, more than 50 data scientists are working on the shop floor. By 2021 we want to integrate all the shops through this process so that we can predict what could happen. An example of how digitalisation in Industry 4.0 is helping us is in the breaking of equipment; whenever the vacuum levels start going up, the machine stops. To avoid this, by digitalisation we can constantly monitor the control limits to ensure that the equipment works in the programmed range. If it goes beyond the safe level, the system sends an SMS to the maintenance team. This helps the operator to plan and change the machine to a new area.”
Energy Conservation
HMI has completely switched over to LEDs, saving about 40 percent energy required for lighting. “Within 18 months we were able to get back the cost of the whole system. We always ensure that energy efficient motors are used. We are also very careful in using water, especially in places like Chennai where water is scarce. We are into hundred percent rain water harvesting. One mm of rain means a saving of 750 kl of water throughout the plant. We can manage 150 days of production without water from other sources; we are planning for complete independence,” he said. (MT)
Hyundai Bayon To Feature 69% High-Strength Steel Grade For Enhanced Safety
- By MT Bureau
- October 21, 2026
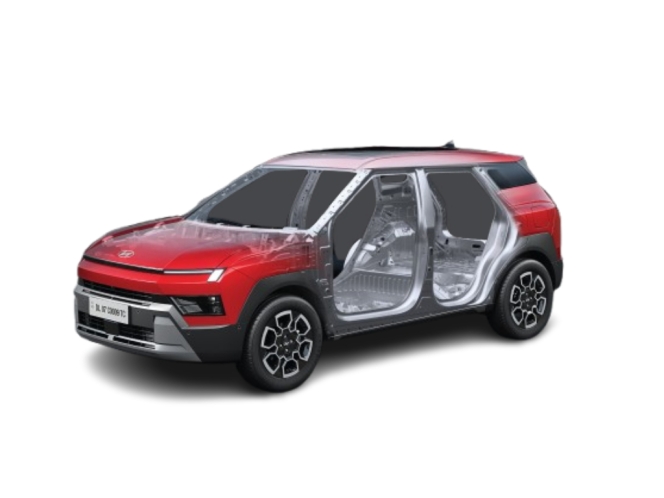
Hyundai Motor India, one of the leading passenger vehicle manufacturers, has detailed the safety specifications and platform architecture for its upcoming Bayon SUV model ahead of its official launch in India on 26 October 2026.
Built on the Global K Enhanced Platform, the Bayon utilises a body structure comprising of 69 percent high-strength steel grades, integrating hot-stamped components across the front apron, dashboard, rear floor and side reinforcements.
The vehicle incorporates Hyundai SmartSense Level 2 Pro ADAS, providing 23 driver assistance features supported by three radar units and 12 parking sensors. Over 35 safety features are fitted as standard across all variants, including six airbags, electronic stability control, hill-start assist control, a tyre pressure monitoring system (TPMS) and ISOFIX child seat anchors.
The Bayon will be powered by a 1.5-litre MPi four-cylinder petrol engine producing 84.4 kW (115 PS) and 143.8 Nm of torque, paired with a six-speed manual or an Intelligent Variable Transmission. Exterior options will span 10 colour configurations across monotone, dual-tone, and matte finishes.
Tarun Garg, Managing Director and Chief Executive Officer of Hyundai Motor India, said, "At Hyundai, we believe that true innovation is meaningful only when it enhances the everyday experiences of our customers. With the Hyundai BAYON, we have combined a robust body structure, advanced safety technologies, and intelligent driver assistance systems to deliver a comprehensive safety experience. From its reinforced chassis and high-strength steel construction to Hyundai SmartSense Level 2 Pro ADAS, the BAYON is engineered to inspire confidence not only in challenging situations, but throughout every journey. This reflects our commitment to delivering intelligent mobility solutions that are safe, connected, and progressive for modern India."
Mitsubishi Motors Launches All-New Pajero In Thailand Ahead Of Global Rollout
- By MT Bureau
- October 21, 2026
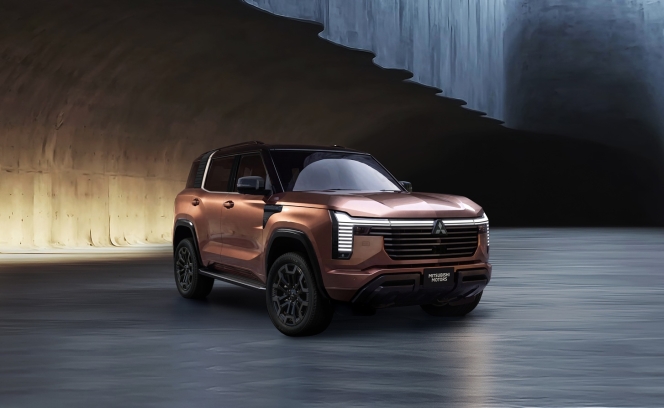
Japanese automotive major Mitsubishi Motors has commenced sales of the Pajero cross-country SUV in Thailand, serving as the initial market for the model’s international release.
The Pajero’s production takes place at the Laem Chabang facility operated by Mitsubishi Motors in Chonburi Province, which functions as a manufacturing hub for export operations.
Shipments to Australia and Japan are scheduled ahead of market releases in mid-December, followed by sequential introductions across approximately 100 countries and regions in the Middle East and Latin America starting in fiscal 2027.
The Pajero integrates four-wheel-drive capability with passenger car handling characteristics and positioning as a flagship offering.
Keisuke Kishiura, President and Chief Operating Officer, Mitsubishi Motors, said, "We are delighted to begin sales of the all-new Pajero in Thailand as the first market for its global rollout. Thailand is not only an important market for Mitsubishi Motors, but also a key hub for our production and exports. The all-new Pajero is a flagship model that embodies Mitsubishi Motors and is positioned among the top-tier cross-country SUVs in the Thai market. We will continue to deliver appealing products from Thailand to customers around the world and provide value that exceeds expectations."
Param Automotive Inaugurates Upgraded Mahindra Showroom In Ahmedabad
- By MT Bureau
- October 20, 2026
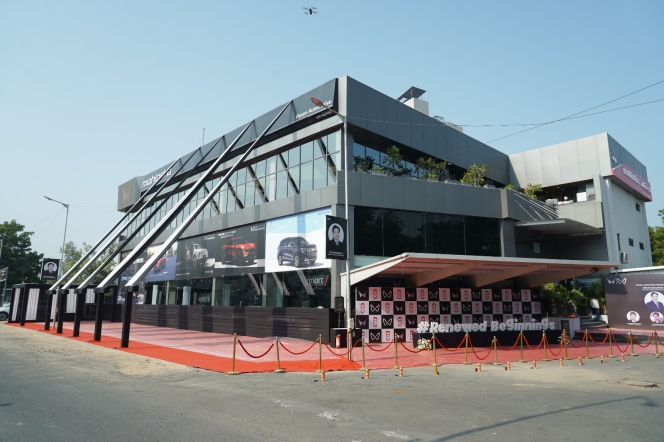
Param Automotive Group has inaugurated an upgraded dealership facility in Ahmedabad to mark its silver jubilee year.
Located at the site established in 2002, the facility spans 40,000 square feet and features display space for 18 vehicles.
The showroom includes customer lounges, delivery zones, accessory bays, test-drive areas and hospitality spaces to support vehicle sales and customer service operations.
BMW Group Expands Lucknow Facility To House MINI Brand Operations
- By MT Bureau
- October 19, 2026
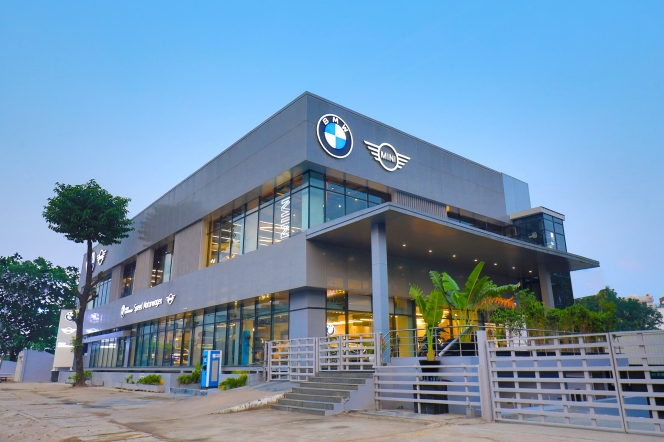
BMW Group India has integrated the MINI brand into its Speed Motorwagen dealership in Lucknow, creating a multi-brand retail facility representing BMW, MINI and BMW Motorrad under one roof.
The Retail.NEXT facility is spread across a 12,142-square-foot showroom for BMW and MINI alongside a 2,088-square-foot pre-owned vehicle display area. The showroom accommodates eight BMW vehicles, three certified pre-owned units and two MINI vehicles.
The site also includes a 2,100-square-foot BMW Motorrad display area featuring 11 motorcycles, supported by dedicated service workshops comprising mechanical, electrical and programming bays. MINI's introduction in Uttar Pradesh aligns with the brand's national retail footprint, which spans 18 sales touchpoints across 17 cities.
Hardeep Singh Brar, President and CEO, BMW Group India, said, "Lucknow is an important luxury market, with customers increasingly seeking brands that reflect their individuality and aspirations. Since 2012, BMW has shaped this market through a compelling portfolio, exceptional experiences and a strong local presence. We lead the luxury electric vehicle segment in Uttar Pradesh, reflecting the growing preference for progressive, sustainable mobility and the strength of our electric portfolio. MINI with its unmistakable style, spirited performance and distinctive character, is a natural fit for Lucknow’s refined taste and appreciation for self-expression. Together with Speed Motorwagen, we are strengthening the power of choice by bringing BMW, MINI and BMW Motorrad under one roof, supported by personalised attention and seamless ownership support."
Divij Narain, Dealer Principal of Speed Motorwagen, said, "The arrival of MINI marks a significant milestone for Speed Motorwagen and discerning automotive enthusiasts in Lucknow. Alongside BMW’s progressive luxury and BMW Motorrad’s spirit of freedom and adventure, MINI adds a distinctive new dimension to our portfolio. Our team is committed to bringing each brand to life through thoughtfully curated product discovery, expert consultation and comprehensive aftersales care. We look forward to nurturing passionate communities across all three brands and ensuring every customer interaction is as memorable and individual as the mobility experience they choose."
Comments (0)
ADD COMMENT