ESI Emphasises On Results, More Than Products: Emmanuel Leroy
- By MT Bureau
- June 22, 2021
OEMs are facing new challenges to improve the existing technologies and develop next-generation ones for the new mobility in shorter times. Reducing market responding time along with new complexities are paving the way for virtual simulation, which displaces physical tests and prototypes by virtually replicating product development, testing and manufacturing with simulations. Emmanuel Leroy, Executive Vice-President Industry Solutions at ESI Group, explains, “We enable our customers to drastically reduce every additional physical prototype by using our solutions. In the end, only one physical prototype is required to validate the whole concept. We envision that one day we may be able to virtually certify a product from end to end.” Excerpts:
 Q) How did the Covid impact the software and services businesses of ESI Group?
The Covid pandemic has accelerated the need for more digitalisation within the industrial market. It has also somehow accelerated the readiness level of our customers and made solutions such as virtual prototyping even more relevant. Indeed, we enabled the continuity of our clients’ business. The use of virtual prototyping allowed them to continue designing, testing and prototyping their products. Our human-centric approach – one of ESI Group’s four outcome solutions – was particularly used by our customers to ensure the continuity of their businesses: using virtual reality to experience the product from home.
During pandemic times, we also provided our CFD (computational fluid dynamic) solutions to help investigating different scenarios to demonstrate the effect of occupant proximity, ventilation systems and contamination avoidance unique to each office and plant environment. ESI Group developed different virtual scenario, based on its facilities in India, to optimise the return to offices and on plant – especially on a car assembly line.
How the growing complexity of part process is influencing the virtual testing?
We notice that the automotive industry is facing more and more draconian regulations, disruptive technologies, intensifying competitions and shortening response time. Coupled with these, customers are getting more demanding on quality, reliability, safety and production deadlines in the business. Indeed, end users are no longer looking for products but for results (flight hours instead of engines, number of possible kilometres instead of electric car, etc.) and they seek for committed and responsible automakers to motivate their buys. At ESI Group, we have understood these preoccupations and we have defined four primary solutions answering our customers’ expectations.
 The first one is the Pre-certification and Validation, enabling gains in performance and productivity. The purpose is double: meeting certification and validation requirements like crash, safety and fatigue issues in the first attempt and then increasing productivity with predictive models and process automation.
The second outcome is Smart Manufacturing, which enables to establish the right manufacturing processes to meet the performance indicators for industrial products and processes.
The Human-Centric Product and Process Validation, our third outcome, focuses on humans by implementing an operator-centric approach to ensure the efficiency of assembly, maintenance operation and the safety of human interactions.
The last one, Pre-experience, is the most advanced solution of ESI Group. Here, our customers and the operators do not look at the product itself, but virtually experience a product, component, subsystem or system under numerous conditions and environments.
Using these approaches, we identify industry challenges from the customer’s perspective and support them in achieving their results.
Finally, as products are getting more complex, one of our strengths is our end-to-end multi-material assembly solution with modelling of different materials (steel, aluminum, composite) and manufacturing processes, covering all the product development cycle.
What will be the growth drivers for the internal combustion engine-driven vehicles business?
Safety is essential and will remain a key driver in the future. Today, the active safety is gaining traction owing to the regulations and overall trends. There is an increasing demand for smart integrated safety, which caters to both active and passive what?
Alongside there are regulations on Co2. In Europe, the Worldwide Harmonised Light Vehicle Test Procedure (WLTP) Norm is challenging and will eventually be implemented in other countries. Regarding Co2 reduction, we focus part of our research and innovation around engine efficiency, aerodynamics and light-weighting, as we did with Bentley for instance.
OEMs are also looking to reduce the manufacturing cost and development time which are leading demand for virtual prototyping, digital twin and shifting OEMs’ investment from hardware to software. The end-to-end value and the digital continuity from the early design to the production is essential to achieve these goals.
OEMs are exploring possibilities to manufacture ICE vehicles and EVs on the same line. Being a solution provider for the smart manufacturing process, how do you see this as a challenge?
Some OEMs assemble EV and ICE vehicles on the same line and look for flexibility, while others use completely dissociated platforms. We, consequently, must find the right strategy regarding their requirements. The new upcoming challenges in CASE mobility manufacturing will bring even more complexities from components to manufacturing. We have to consider the complexity to train the operators: our virtual reality solutions are key here. We help our customers by providing training, on both ICE vehicles and EVs manufacturing processes to their team, even from different place around the world, gathered on the same interface. This solution gathers all stakeholders (from operators to QHSE officers and plant managers) around the same product. This immersive tool helps getting complementary feedbacks early on in the process.

Where do you find more competencies or comfortability — in the complete vehicle design or component design?
Clearly, we are positioning ourselves on the whole vehicle design as it gives the most significant benefit for the OEM and other customers. We are talking about an end-to-end value that we can demonstrate on full scale CAE demonstrators. When it comes to a standalone component, the complex interactions between components and environment are not well taken into account and can lead to reduced predictiveness. In this case, we come up with a holistic view of the problem itself. It is how we defined the four outcome solutions introduced earlier.
Do you think that virtual prototypes will, at a 100 percent, completely replace physical ones ?
Virtual prototypes are step by step replacing physical prototypes. Nevertheless, I think physical prototypes remain today essential to certify the product at the very end of the development phase. To give an example, in 2019 Renault succeeded a 5-star rating of its Clio 5 on the Euro NCAP safety certification test with a single physical prototype, the one needed for the consumer test. Virtual certification is a topic discussed within the automotive ecosystem, allowing to solely relying on the simulation from end to end. But we are not at that point right now.
Which is your largest market for automotive business?
The automotive industry is the most significant contributor to our total revenues. Today, Japan is the largest market for our automotive business. However, India has been an important market for ESI, and it has been growing quite well over the years.
Most of our engineering developments teams, for both our software and our platforms, are based in India.
What are the challenges in the business?
The increasing complexity I mentioned before is definitely a challenge, but it also brings opportunities to us. Our end-to-end multi-material, multiprocess solutions and chaining capabilities are key to overcome the challenges of the automobile market. Due to the ever growing content of electronics, system simulations and systems of systems techniques are improving as well. Our focus is to strengthen our collaboration with partners in the ecosystem to support the customers in solving their complex problems. (MT)
BendPak Pays Tribute To US Armed Forces With Valor C10 Debut At 2026 SEMA Show
- By TT News
- November 12, 2026
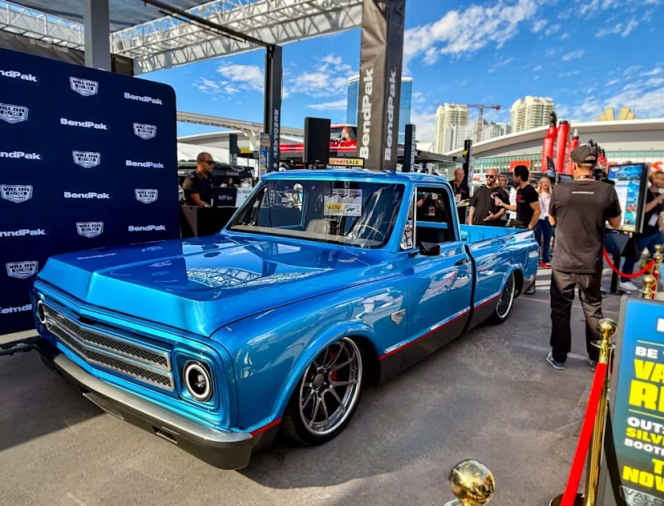
BendPak Inc. unveiled the Valor C10, its first custom-built vehicle, at the 2026 SEMA Show. The handcrafted 1970 Chevrolet C10 pickup honours the sacrifice, courage and commitment of the US Armed Forces. Its debut coincided with Veterans Day, lending the salute added poignancy for the company and its staff.
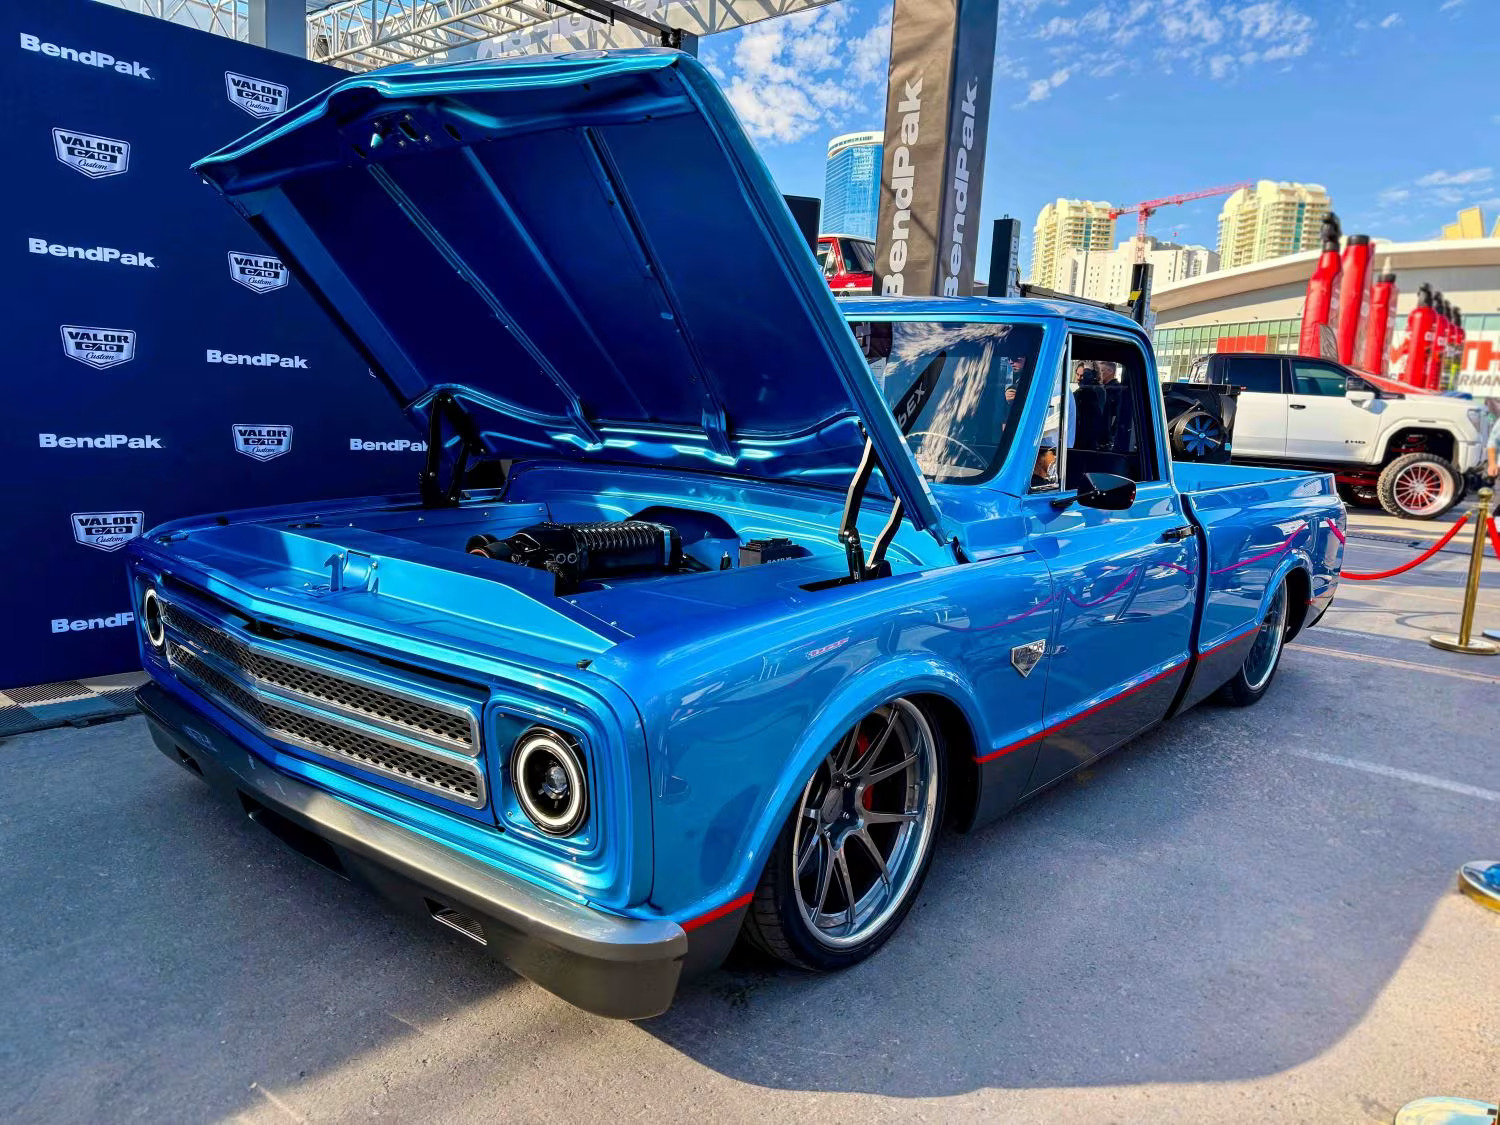
The truck fuses contemporary performance with enduring design, reflecting the American strength, ingenuity and resilience shared by BendPak and the military. Nostalgia Hot Rods, under Dustin Hacker's direction, handled the build, starting with a vintage C10 and retaining little beyond a heavily modified cab. The body-dropped pickup keeps over 4.5 inches of usable ground clearance despite its slammed stance, thanks to Hacker's chassis work. Metallic blue paint with red accents – a body stripe, brake callipers and engine – echoes the US flag, blue for vigilance, perseverance and justice, red for hardiness, sacrifice and the valour behind the truck's name.
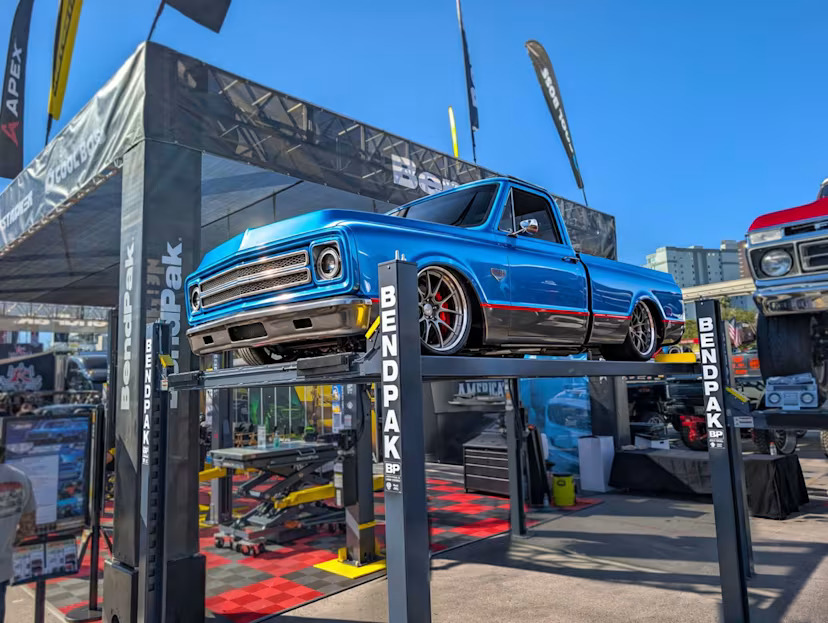
BendPak's creative team designed custom Valor C10 badges for both doors, and the cabin pairs a classic bench seat in two-tone gray Alcantara with blue stitching against bespoke door panels and headliner. Power comes from a BTR Gen V Stage 2 supercharged camshaft, a custom 3.5-inch aluminium driveshaft, MagnaFlow 3-inch mufflers and a Holley Terminator X Max engine management system. A Gearstar GM 6L80E six-speed automatic, a custom Eddie Motorsports serpentine system, a Speedtech Extreme G chassis and QA1 four-way adjustable coilovers with cantilever rear suspension complete the mechanical package, alongside Forgeline custom wheels, JL Audio C7 components, a Kenwood 6.8-inch head unit, a PCS electronic gear shift module with wireless paddle shifter, Dapper Lighting custom headlights and taillights in billet housings,and Nu-Relics power windows.
Military service runs deep at BendPak. Founder Don Henthorn, a US Army veteran, started the company in 1965. President and CEO Jeff Kritzer served three years on active duty as a US Air Force C-130 loadmaster before joining the Air National Guard, preserving his flight status and loadmaster duties while launching his BendPak career – a taxing dual role he upheld for three years. He is the son of a senior master sergeant and fellow loadmaster devoted to military service, and his son Devin served with distinction in the US Army, including deployments to the Gulf region and Bangladesh.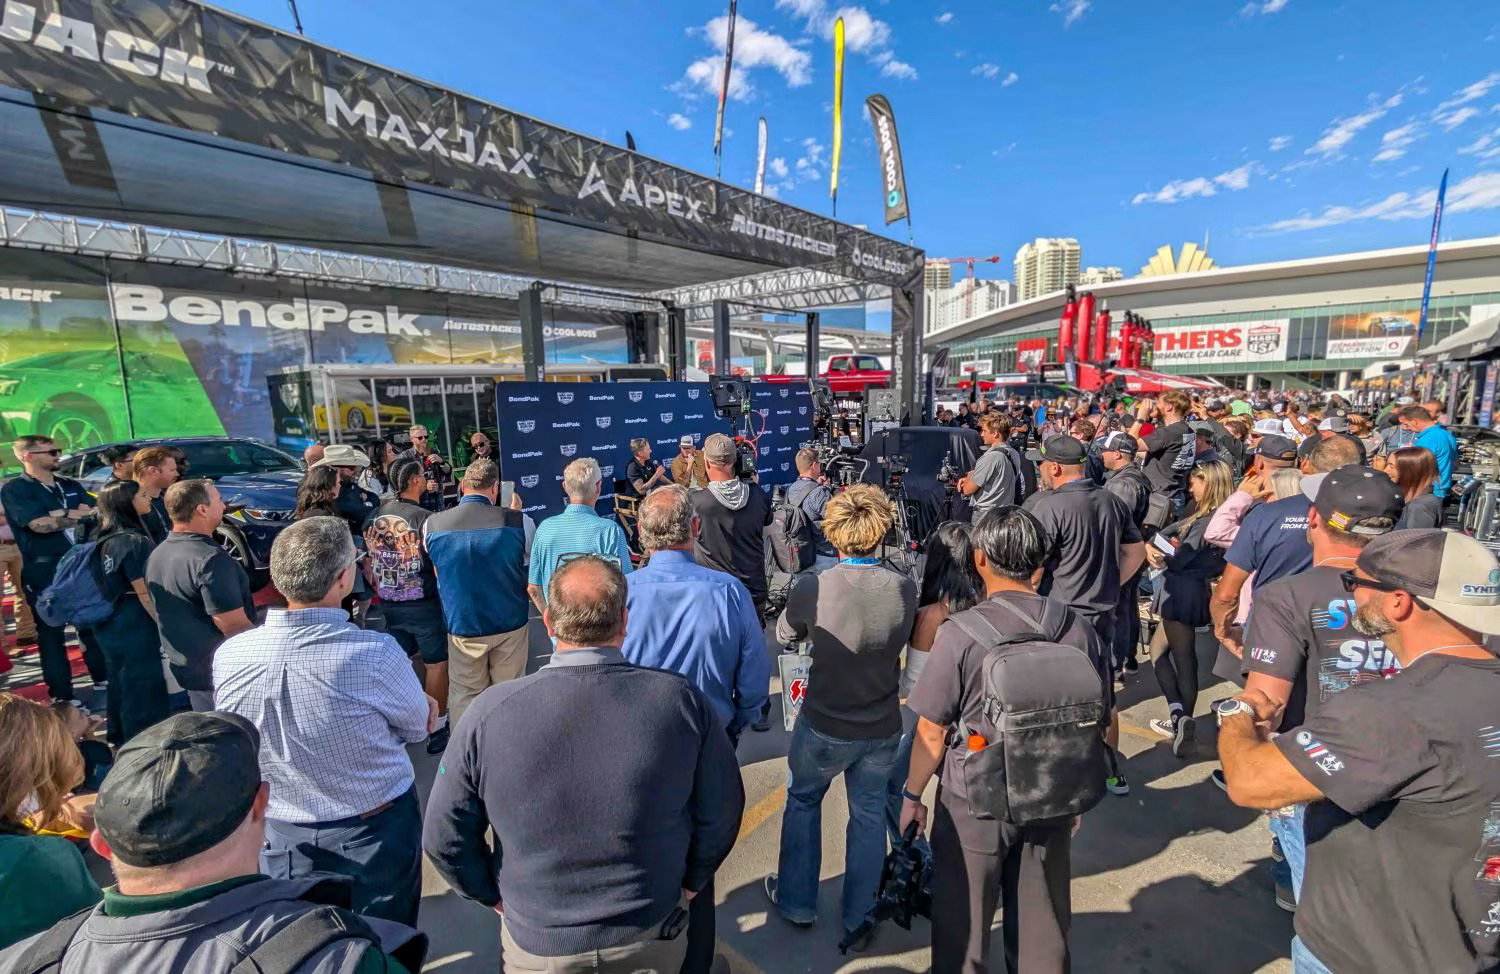
Kritzer said, “We call this build the Valor C10 – it was created to honour the brave men and women who have served and continue to serve in our armed forces, especially those who gave their lives in defence of our nation. BendPak proudly supports the military community. This serves as our way of saying thank you and reminding everyone that freedom isn’t free.”
Sean Price, Director of Product Development, BendPak, said, “We’ve worked with Dustin for several years, supplying his shops with BendPak lifts and equipment, as well as showcasing many of his amazing builds in our SEMA Show booths. We knew he had the passion and craftsmanship to bring our vision for the Valor C10 to life.”
Hacker said, “Most of the sheet metal is custom-fabricated, including the roof, hood, drip rails, floors, bumpers, engine bay and bed. Under the hood, there’s a 376-cubic-inch V8 with a 2.9-litre Whipple supercharger. This thing will make 750 horsepower and drive like a dream.”
ContiTech Invests In Pune Surface Solutions Site With Colour Lab And Prototype Facilities
- By MT Bureau
- November 12, 2026
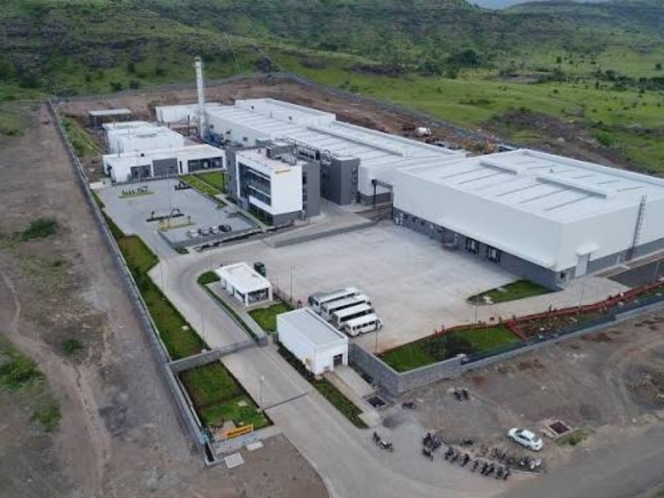
ContiTech is expanding its research and development capabilities at its Surface Solutions facility in Pune through investments in a dedicated Colour Lab and prototype development infrastructure, alongside the addition of four roles to its local engineering team. The company has also appointed Alok Pandey as Head of Plant Management Pune to oversee site operations.
The Colour Lab will handle colour development, colour matching, appearance evaluation and material testing for vehicle interiors. While primarily serving automotive manufacturers in India, the facility will also support development projects across the Asia-Pacific, Europe, Middle East, and Africa regions. Coupled with prototype testing equipment, the site will enable validation of surface materials for passenger cars and two-wheelers.
Alexander Scholz, Head of Business India, Surface Solutions at ContiTech, said, “India is a key growth market for our business and an important pillar of our long-term development strategy. As automotive manufacturers increasingly seek localised development support, faster response times and closer technical collaboration, these enhanced local capabilities will help us better support our customers' evolving needs. This investment reinforces our ‘In India, for India’ approach and reflects our confidence in the continued growth potential of the Indian automotive industry.”
Burak Uzel, Head of Design, Surface Solutions at ContiTech, said, “Automotive interiors have become a key differentiator for vehicle brands. Customers increasingly expect premium, comfortable and individualized interior experiences, while OEMs seek innovative and sustainable material solutions. This investment will strengthen our ability to develop and validate colour concepts locally, enabling closer collaboration with customers and supporting the next generation of interior design and material solutions for the Indian market.”
Jan-Philipp Behrndt, Head of Operations Automotive Plants, Surface Solutions at ContiTech, said, “The expertise and dedication of our local teams are key to our success. With the planned expansion of our R&D organization, enhanced technical capabilities and strong local leadership, Pune will continue to grow as an important contributor to our global innovation network. I am confident that the team's expertise and commitment will support our future growth and create additional value for customers.”
Kia India & Suppliers To Invest $2 Billion For 2nd Plant In Andhra Pradesh
- By MT Bureau
- November 12, 2026
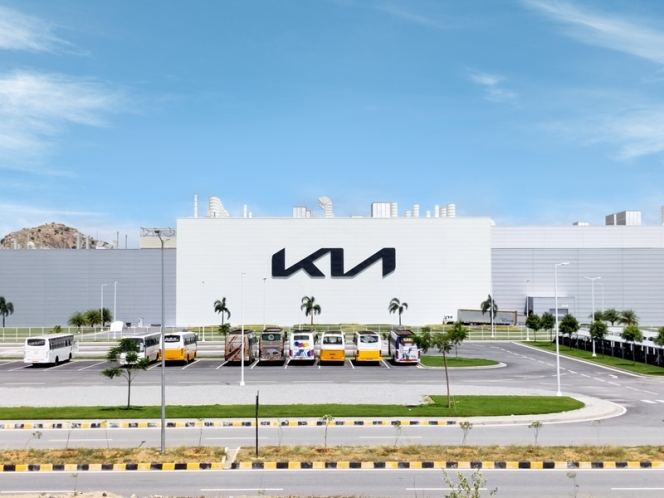
South Korean auto major Kia India and its supplier partners will invest USD 2 billion to establish a second manufacturing facility in Anantapur, Andhra Pradesh, following the signing of a Memorandum of Understanding with the Government of Andhra Pradesh.
The new facility is scheduled to commence production in early 2030. It will add an annual installed capacity of 200,000 units, taking Kia India's combined production capacity beyond 600,000 units per year.
Spread across 465 acres for Kia and its suppliers, the facility will handle stamping, welding, painting and assembly operations for models across internal combustion engine and electric vehicle powertrains.
The project is expected to generate approximately 12,000 direct and indirect employment opportunities, adding to the 24,237 personnel employed across the company's existing 945-acre plant, which holds a production capacity of 430,000 units annually. With the addition of this facility, cumulative investments by Kia and its suppliers across both plants in the state will reach USD 5 billion.
Gwanggu Lee, MD and CEO, Kia India, said, “India is central to Kia’s long-term growth ambitions, and the trust our customers have placed in us since we began operations in Anantapur has been instrumental in our journey. Our second manufacturing plant marks a significant new chapter, strengthening our ability to respond to customer demand with greater speed and flexibility, while supporting the introduction of new models across ICE and EV powertrains. As we enter our next phase of growth, we remain committed to contributing to India’s automotive ecosystem and building on the strong foundation we have created here. This will further expand our Made-in-India footprint, strengthening our ability to serve both domestic and overseas markets.”
Ultraviolette Automotive Ropes In Royal Enfield’s Abhijit Singh Brar As Head Of Marketing
- By MT Bureau
- November 12, 2026
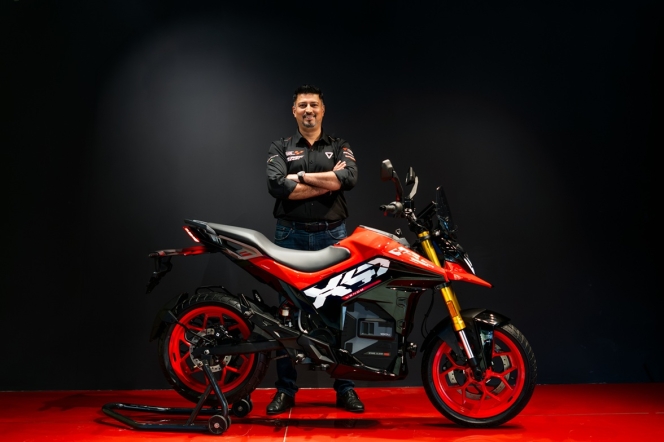
Bengaluru-based electric two-wheeler manufacturer Ultraviolette Automotive is strengthening its senior leadership with the appointment of Abhijit Singh Brar as Head of Marketing.
In this role, Brar will oversee brand positioning, product launch strategies and demand generation as the electric motorcycle manufacturer expands its product portfolio across India and export markets.
Brar brings more than two decades of experience across consumer and automotive sectors. He previously spent over eight years at Royal Enfield, where he established the domestic marketing function and subsequently led marketing operations across Europe, North America, Australia, Latin America and Southeast Asia, managing product introductions and market entries.
Prior to joining Ultraviolette, he held marketing and business strategy positions at Lodha, following earlier brand and commercial leadership roles at Bacardi and Diageo.
Narayan Subramaniam, CEO and Co-Founder, Ultraviolette Automotive, said, "We are excited to welcome Abhijit to Ultraviolette at a significant stage in our growth journey. His role in shaping Royal Enfield's brand journey and supporting its successful expansion across global markets will be particularly valuable as we broaden our product portfolio and reach new segments of riders. Alongside his extensive experience across consumer industries, he brings a deep understanding of consumer aspirations and a proven ability to build brands at scale. We look forward to leveraging his expertise to further strengthen Ultraviolette's position and accelerate our next phase of growth in India and international markets."
Comments (0)
ADD COMMENT